Die Casting Tolerances - CT Classes & Dimensions
Complete die casting tolerances guide: ISO 8062 CT grades, linear dimension tables, hole position, flatness, and machining allowance recommendations.

Technical Director, Die Casting Engineering
Blog Visual Plan
Article visuals for die casting tolerances
These visuals use your current KastMfg image library now, and they will automatically switch to article-specific images when you add them later.
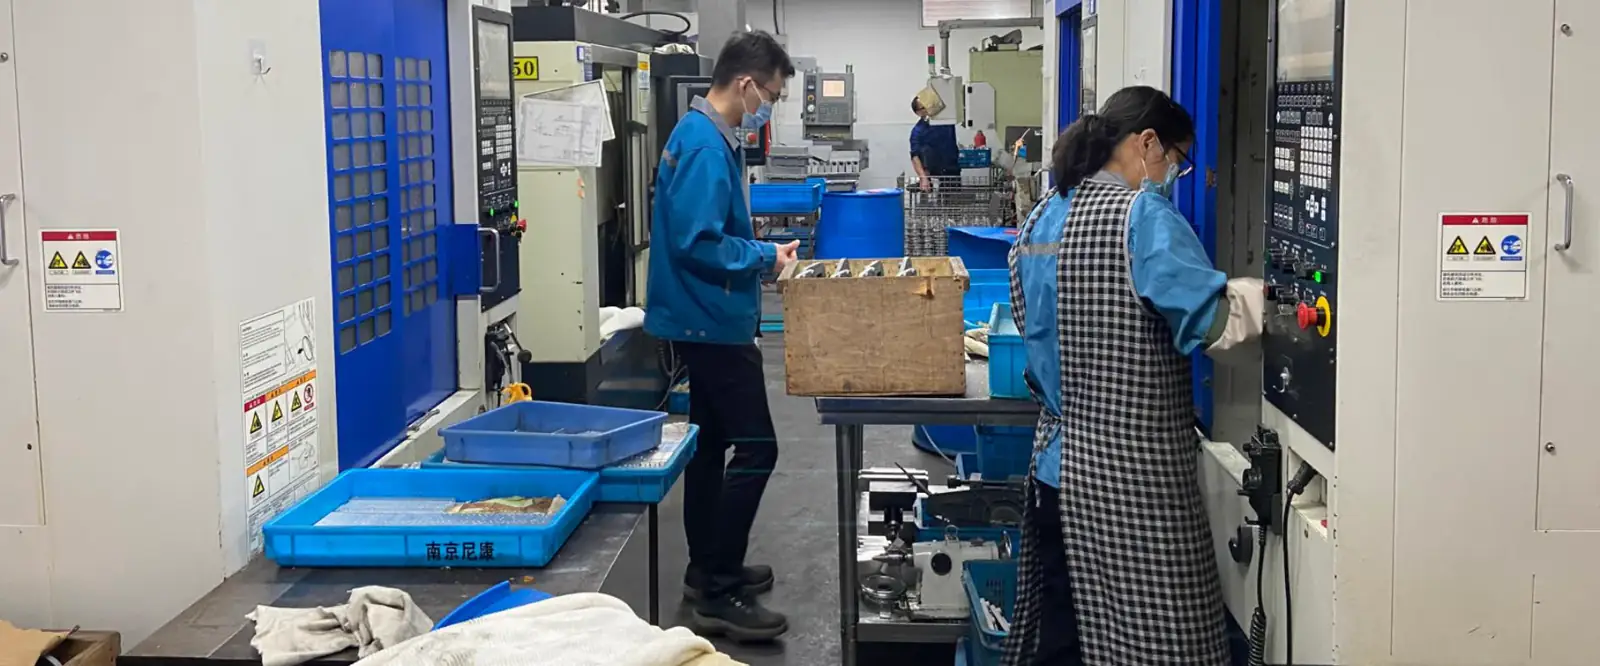
Lead Technical Image
Add a hero-level manufacturing, tooling, or component image that reinforces the article topic above the body copy.
Comparison or Detail Image
Reserve a second image for an alloy comparison, defect example, tooling detail, or application close-up deeper in the article.
Engineers specify tolerances based on function. Die casting suppliers quote based on process capability. When these two perspectives are not aligned — when a drawing specifies CNC tolerances (+/-0.05 mm) on as-cast features — the result is either excessive cost or quality rejection.
ISO 8062 CT Grades
ISO 8062 defines Casting Tolerance (CT) grades CT1 (most precise) to CT16 (least precise). Die casting achieves CT3-CT6:
| Process | Typical CT Grade |
|---|---|
| Zinc HPDC | CT3-CT5 |
| Aluminum HPDC | CT4-CT6 |
| Magnesium HPDC | CT4-CT6 |
| Low-pressure die casting | CT5-CT7 |
| Sand casting | CT11-CT13 |
CT Grade Tolerance Values (mm on linear dimensions)
| Nominal dimension (mm) | CT4 | CT5 | CT6 | CT7 |
|---|---|---|---|---|
| up to 10 | +/-0.16 | +/-0.26 | +/-0.36 | +/-0.52 |
| 10-25 | +/-0.20 | +/-0.32 | +/-0.44 | +/-0.64 |
| 25-63 | +/-0.26 | +/-0.40 | +/-0.56 | +/-0.80 |
| 63-160 | +/-0.36 | +/-0.52 | +/-0.76 | +/-1.10 |
| 160-250 | +/-0.44 | +/-0.64 | +/-0.90 | +/-1.30 |
| 250-400 | +/-0.52 | +/-0.78 | +/-1.10 | +/-1.60 |
Feature-Specific Tolerance Guidance
Parting Line Features
Dimensions crossing the parting line are 1-1.5 CT grades worse than same-half dimensions due to die alignment variation. Design critical dimensions to fall within one die half.
- Flash thickness after trimming: 0.05-0.15 mm
- Die mismatch at parting line: 0.10-0.30 mm
Ejector Pin Marks
Depressions or protrusions 0.05-0.20 mm at ejector pin locations. KastMfg places ejector pins on non-functional, non-cosmetic surfaces — identified during DFM review.
Holes and Bores
| Feature | As-cast | Post-machined |
|---|---|---|
| Hole diameter | +/-0.10-0.30 mm | H6/H7: +/-0.005-0.015 mm |
| Hole position | +/-0.20-0.50 mm | +/-0.05-0.10 mm |
Flatness
| Condition | Achievable |
|---|---|
| As-cast flat surface | 0.1-0.5 mm |
| CNC face-milled | 0.01-0.05 mm |
| Ground sealing face | 0.005-0.01 mm |
CNC Machining — Extending Tolerance Capability
| Feature | As-Cast | Post-Machined |
|---|---|---|
| Linear dimensions | +/-0.15-0.5 mm | +/-0.02-0.05 mm |
| Bore diameter | +/-0.1-0.3 mm | +/-0.005-0.015 mm |
| Flatness | 0.1-0.5 mm | 0.01-0.05 mm |
| Surface roughness | Ra 1.6-3.2 μm | Ra 0.4-0.6 μm |
| Thread | Not recommended as-cast | M3-M30, gauge-verified |
Economic principle: Specify as-cast tolerances wherever function permits. Reserve machining for features where tighter tolerance adds genuine value. Over-tolerancing a die casting adds 15-30% to part cost unnecessarily.
How to Specify Tolerances on a Die Casting Drawing
- Use a general tolerance note: "All untoleranced dimensions per ISO 8062 CT5"
- Call out tight tolerances explicitly only on features that functionally require them
- Identify parting line location and ejector pin placement restrictions
- Mark cosmetic surfaces (for gate placement guidance)
- Mark pressure-critical surfaces (no porosity)
Common mistakes to avoid:
- Specifying +/-0.05 mm general tolerance on a casting drawing
- Not identifying the parting line location
- Specifying flatness of 0.02 mm on an as-cast surface without machining callout
GD&T on Die Castings: Datums, Profile, and the Two-Drawing Question
The guidance above is about which values to write down. Just as consequential is the framework they hang from: which features serve as datums, how a general profile treats an as-cast surface, and whether casting and machining live on one sheet or two.
The CAD Model as Master Dimension
A newer practice declares the 3D CAD model the master dimension and controls every surface with a general profile-of-a-surface tolerance, instead of a 2D drawing full of plus/minus dimensions. One supplier push-back case worth understanding: a buyer annotated a whole high-pressure die casting this way at a general profile of 0.8; the supplier asked to open it to 1.2. Neither figure is correct in the abstract. A general profile on an as-cast part absorbs everything the process varies with — part size, parting-line crossings, die wear over a run — so the defensible number lands somewhere between design intent and caster capability, and it closes in DFM review, not a drawing standoff.
Choosing Datum Features on an As-Cast Part
Casting datums should be features the die reproduces identically every shot. The pattern argued out in an automotive-casting thread: a stable as-cast plane as primary, then two as-cast holes — spaced as far apart as the part allows — as secondary and tertiary, so casting variation rotates the part least at inspection. A machined feature fails as a casting datum: it does not exist when the casting is inspected, and if machining changes supplier or stock allowance, the reference disappears. Machined features reference cast datums, never the reverse.
Passing Datums From Casting to Machining
A machined box housing shows the chain: the casting carries three mutually perpendicular datum references — a face and two holes, all as-cast — and the first machining operation picks them up to establish the machined datum scheme everything else chains from. Keep the chain intact and wall thicknesses land where the model says; break it — first operation indicated off a convenient surface instead of the cast datums — and every downstream position and profile tolerance pays for the shift.
One Drawing or Two
A part with little machining can carry as-cast and machined dimensions on one sheet. Past that, the cleaner architecture is two: a casting drawing for the as-cast state, a machining drawing for the finished part, the casting datum features carried across in phantom lines so the two stay explicitly related. That convention is what ASME Y14.8, the US standard for casting and forging drawings, exists to govern — the reference to name when the practice needs backing. The habit prevents the mixed sheet, where foundry and machine shop each read the tolerances that suit them.
FAQ
Can die casting achieve +/-0.02 mm without machining?
For feature-to-feature dimensions within the same die half, CT3 zinc achieves approximately +/-0.05-0.10 mm for small features. Reaching +/-0.02 mm consistently requires CNC machining.
How do I specify die mismatch on the drawing?
ASME Y14.8 covers it directly: clause 3.13, Mismatch, states that mismatch "where applicable, shall be specified as a maximum value." In practice that means one added note on the casting drawing — a maximum mismatch value, applied to dimensions that cross the parting line — rather than burying the allowance inside the general tolerance. Dimensions within one die half do not need it; they cannot mismatch. Buyer-side, this note is what an incoming-inspection dispute turns on: a casting can be dimensionally perfect in each half yet out of spec as a part, because the halves shifted relative to each other at the parting. Specifying the maximum up front (a common commercial range for small castings is 0.1-0.3 mm on as-cast parting-line dimensions; the defensible number scales with projected area and closes in DFM review) makes that failure mode a measured, quoted quantity instead of a surprise at goods-in.
What tolerance applies to dimensions crossing the parting line?
Approximately 1-1.5 CT grades worse than same-half dimensions. Design critical dimensions within one die half where possible.
When does it make sense to machine a die casting instead of holding tighter as-cast tolerances?
Tighten the casting process first, then machine only what genuinely needs it. As-cast tolerances in the CT4-CT6 range already cover most functional features; CNC machining earns its cost on features that must hold CT3 or better — bearing bores, sealing faces, precise hole positions — or on features that cross the parting line and cannot be held in one die half. Specifying tight as-cast tolerances everywhere raises unit price and scrap risk across the whole part, while machining concentrates cost on the few features that justify it. The practical RFQ approach: mark the truly critical dimensions on the drawing and let everything else float at standard tolerance.
Die casting vs CNC machining from billet — how do I choose?
Volume drives the decision more than tolerance does. Die casting amortizes tooling across thousands of parts and wins on unit cost once volumes justify the mold; CNC from billet has no tooling cost but every part pays full machining time, so it wins for prototypes and low volumes. Geometrically, castings are more rigid for their weight (near-net shape, thin walls possible), while billet allows features a die cannot eject (undercuts, zero draft). Tolerance-wise both can reach the same numbers on machined features — the difference is that on a casting you machine only the critical faces, on a billet part you machine everything.
Tolerance consultation — free with every RFQ: casting@kastdiecast.com | +86 138 1403 4409
Does the drawing's title-block tolerance apply to as-cast dimensions?
A frequent and costly assumption. Title-block general tolerances on a machining drawing are set for machining, and applying them to as-cast features asks the casting process to hold tolerances it was never intended to hold. ASME Y14.8 — the US standard for casting and forging drawings — is the reference for casting-specific dimensioning, and the practice it supports is separating the casting drawing from the machining drawing: as-cast dimensions carry casting-grade tolerances on the casting drawing, and only machined features are controlled by the machining drawing. When the two are mixed on one sheet, the foundry either quotes high to cover the risk or quietly quotes to the casting grade — and disputes follow at inspection.
How much machining stock should I leave on a die casting?
Less than you would on a sand casting, but the honest answer is that stock depends on part size, feature, and the caster's process capability, not a single universal number. The practical route: put the machining allowance question to the caster during DFM review with the datum scheme in hand, and let the drawing reflect what the process can actually hold rather than a textbook figure. What matters for cost is that every machined face is a deliberate decision — stock on a face is machining time, and unmachined faces are free.
What does "within X of basic position" mean on a casting drawing?
Should sealing areas on a die casting be machined, or left as-cast?
Why does my die cast part always show flash at the parting line — is that a tolerance problem?
Should I build the as-cast model first or the as-machined model?
Design-for-manufacturing orthodoxy says model the as-cast part first and derive the machined part from it. The logic: the casting is what the die makes, so the die should be designed around a shape that is manufacturable as a casting — draft, uniform walls, ejector-friendly — and machining then removes defined amounts of stock from that shape. The counter-practice is real and rational too: designers who need the finished part for assembly-level work model the as-machined geometry first (because that is what the product actually is), then build the casting around it by adding machining stock and draft. The friction appears when the two models drift apart in revision control — the machined model gets a fillet the casting never received, and nobody notices until the machined face cuts into a wall the casting did not thicken.
What the drawing package should pin down:
- Which model is master. State it in the title block or revision note. If the as-machined model drives, the casting model must be regenerated from it every revision — mechanically, not by hand.
- The stock map. Which faces get machining stock and how much belongs on the casting drawing, where the caster can quote it. Machining an unmachined face is a scope dispute waiting to happen.
- The datum chain between them. As covered under passing datums from casting to machining: cast datums established first, machining referenced to them. A model pair without a stated datum chain is two shapes, not a part definition.
The workflow choice (cast-first or machined-first) matters less than the discipline connecting them. Either sequence produces good castings when the stock map and datum chain are explicit; both produce scrap when the as-cast model is a stale snapshot of an as-machined model that kept moving.
How should draft affect GD&T callouts on a casting drawing?
Draft puts a taper on every surface perpendicular to the die-open direction, and a tolerance framework that ignores it will argue with reality at inspection. Three practical rules cover most of it.
First, position and profile zones must say where they apply. A drafted hole changes diameter with depth, and a drafted wall is neither a plane nor a true cylinder — so a position callout on a cast hole needs an application point (commonly the datum face or a stated depth), and a profile callout on a drafted face must say whether the zone follows the taper or brackets it. An unspecified measurement location is an invitation for the foundry and the CMM program to disagree.
Second, use draft-included notation deliberately. Casting standards — ASME Y14.8 is the US reference — support a draft-added tolerance, often noted DFT±, meaning the stated tolerance zone is widened by the draft effect in the direction the taper adds metal. It is the honest notation for as-cast surfaces whose function tolerates the taper: the drawing says "this much, plus draft" instead of pretending the face is geometrically true. Where the function needs true geometry — sealing lands, bearing bores — do not paper over draft with a bigger zone; machine the feature and tolerance the machined geometry.
Third, build the datum scheme from surfaces that repeat. Prefer datum features that are stable and reproducible — a machined face, or datum-target points and areas on as-cast surfaces — rather than full as-cast faces that wander with die temperature and wear, and keep the same scheme from casting inspection through machining so tolerance stacks do not shift at every handoff.
Why did my cast part move after machining?
Because you removed part of the balance. A die casting solidifies under non-uniform cooling and holds residual stress locked in its sections; while the part is whole, that stress cancels itself out. Machine a deep slot or take a heavy asymmetric cut, and the material that carried half the stress balance goes into the chip bin — the remaining metal re-equilibrates, and the part bows or twists toward the removed side. Classic symptom from machine shops: a cast aluminum blade holder running out 0.015" over 12 inches after the retaining slot is milled — the slot released the stress, and the "growth" is the casting finding its new equilibrium. The countermeasures are process discipline rather than heroics: remove stock symmetrically where the geometry allows, split roughing and finishing passes so the part settles between them (with a rest or re-clamp strategy that does not spring the part into the fixture), and leave the final critical surfaces for a light finishing pass after everything else has been opened up. Where the tolerance is genuinely tight and the part keeps moving, a stabilization step — thermal stress relief or simply letting roughed parts sit before finishing — is the recognized route, with the caveat that heat treatment options depend on alloy and process (conventional HPDC has its own limits there). This is also why the as-cast vs as-machined model question belongs in DFM: if you know which faces get cut, you can plan removal order before the first chip flies.
Related
- DFM die casting
- surface finish chart - Ra values and process capability
About The Author
Mike Yao on die casting tolerances
Technical Director, Die Casting Engineering
Technical Director at KastMfg with 20+ years in high-pressure die casting, leading engineering and program management across aluminum, zinc, and magnesium programs for automotive, EV, electronics, and medical OEMs worldwide.
View author profileRelated Reading
Keep exploring the blog
Die Casting vs Permanent Mold Casting: Which to Choose?
Die casting and permanent mold casting are both metal mold processes - both use reusable steel or iron dies rather than expendable sand. The difference is how the metal gets in:...
Mike Yao
7 min read
CNC Machining Die Castings: Tolerances & Cost
CNC machining die castings is used when as-cast geometry cannot meet functional tolerances, sealing requirements, bearing fits, threads, flatness, or assembly interfaces. Die ca...
Mike Yao
8 min read
Die Casting Design Guide: Rules, Tolerances & DFM
Good die casting design is the single biggest lever on part cost and quality - more than the alloy, more than the supplier. A part designed for die casting from the start will q...
Mike Yao
5 min read
Die Casting Die Explained - Anatomy, Steel, Life, and Cost
A die casting die is a precision steel mold - typically two machined halves of H13 hot-work tool steel - that shapes molten metal injected into it under high pressure. It is the...
Mike Yao
5 min read