Custom Die Casting Services - Drawing to Delivery
Custom die casting services from DFM review to delivery: in-house tooling, PPAP sampling, production, CNC machining, and finishing for global OEM buyers.
Production Capabilities
Supporting visuals for custom die casting
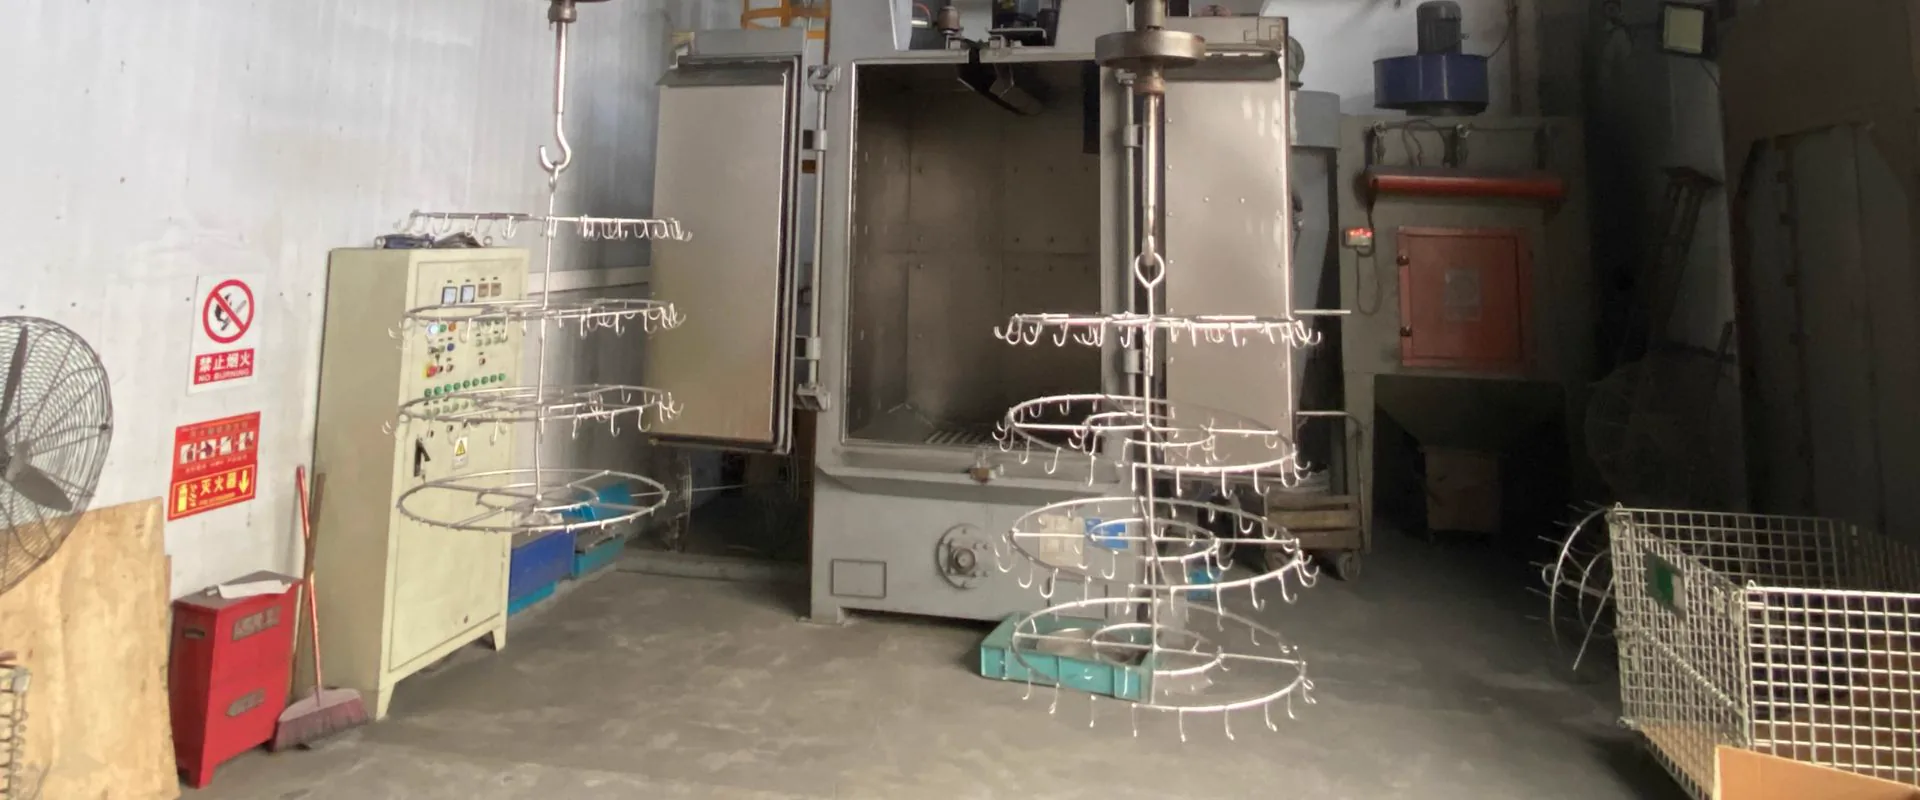
Manufacturing Operations
Die casting production, tooling fabrication, CNC machining, and quality inspection at our Nanjing facility.
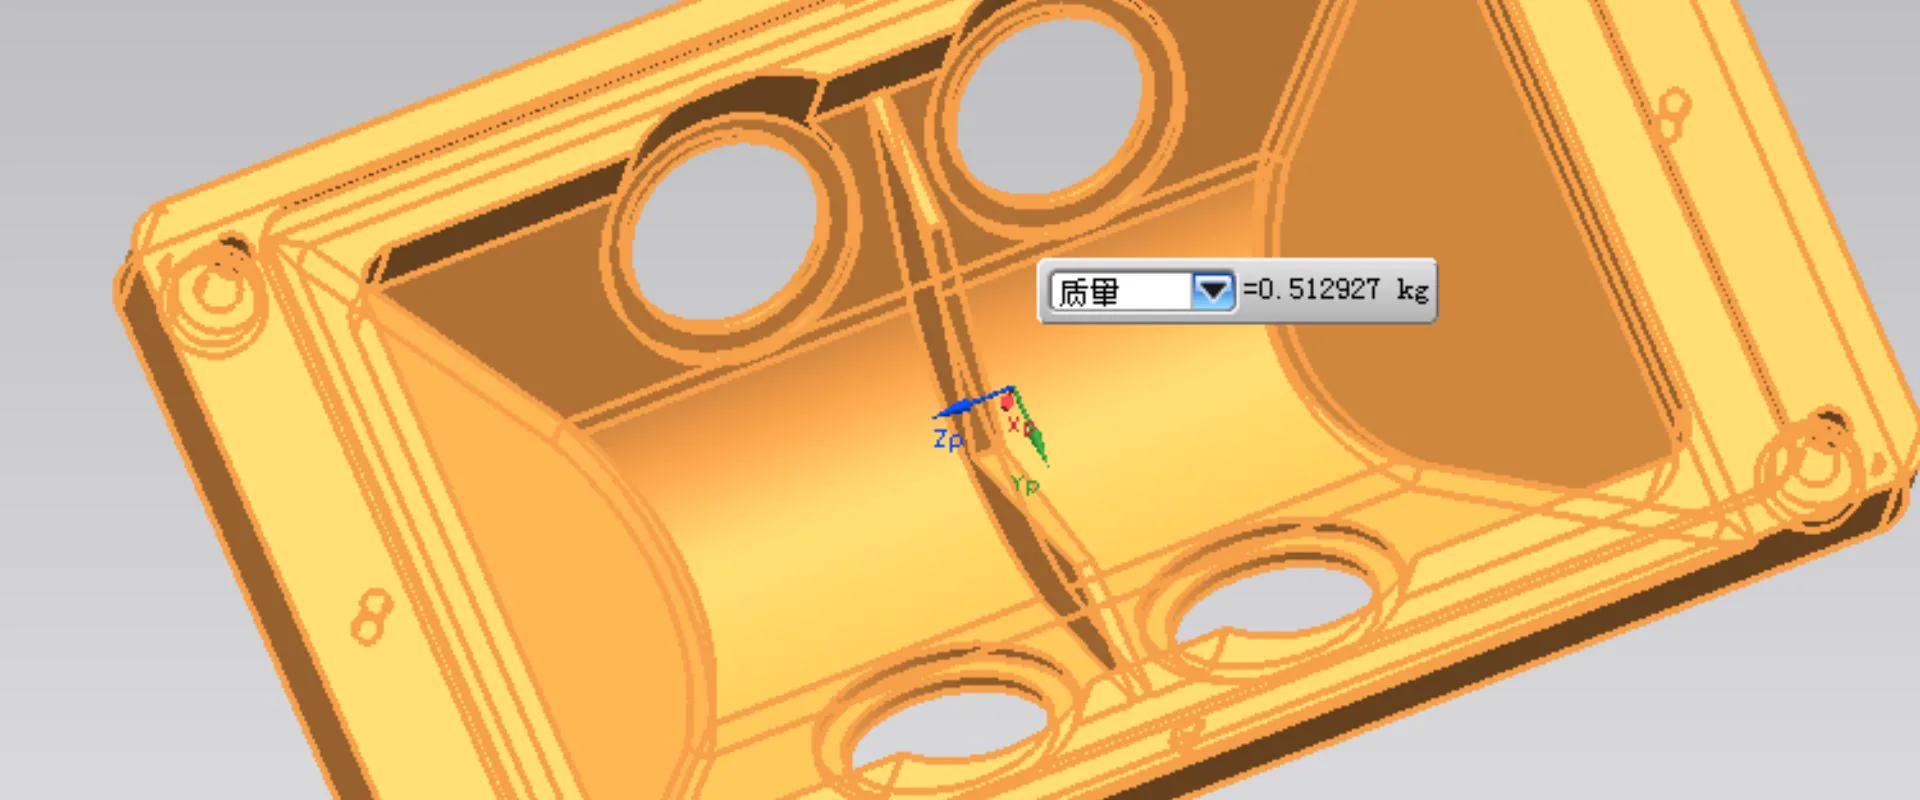
Component Detail
Close-up views of cast components showing surface finish, dimensional features, and application-ready quality.
KastMfg provides a complete custom die casting service for OEM, Tier 1, and industrial customers worldwide. From your first inquiry through DFM review, tooling fabrication, first article sampling, production, and logistics - one team, one facility, one point of accountability.
We have produced custom die casting components for over 20 years, from simple single-cavity aluminum brackets to complex multi-slide zinc parts with electroplated decorative surfaces. Our engineers apply that experience to every new program.
What "Custom" Means at KastMfg
Custom die casting at KastMfg is not a catalog product with your logo on it. It is:
- Your geometry - produced to your 2D drawing or 3D CAD model, with your tolerances
- Your alloy - we recommend the optimal alloy for your application, or work to your specification
- Your quality requirements - ISO 9001:2015 certification, IATF 16949 compliant processes, PPAP, or your own internal acceptance criteria
- Your schedule - tooling and production timelines defined and committed at program launch
Our Service Model
Free DFM Review - Before You Commit to Tooling
Every KastMfg inquiry begins with a Design for Manufacturability (DFM) review at no charge. A project engineer reviews your drawing for:
- Draft angles - surfaces parallel to die opening must have sufficient taper for ejection
- Wall thickness - uniform thickness prevents shrinkage porosity and warpage
- Undercuts - features requiring slides are identified and costed
- Tolerances - we confirm which tolerances are achievable as-cast vs. requiring post-machining
- Gating and overflow - gate location affects surface appearance; overflows capture cold metal
You receive a written DFM report with specific recommendations - if design changes can reduce tooling cost or improve casting quality, we explain what to change and why. Customers have saved thousands of dollars in avoided tooling changes.
In-House Tooling - No Subcontracting
KastMfg designs and fabricates all tooling in our own tool shop. We do not outsource die fabrication. This means:
- Faster lead times - no coordination delays with external tooling shops
- Better quality - the same team that designs your casting advises on the die design
- Full traceability - die drawings, material certs, and maintenance records kept in-house
- Direct control - if a trial shot reveals a fill problem, our tooling team modifies the die on-site the same day
Tooling timeline:
- Prototype die (P20 steel, single cavity): 3-5 weeks
- Production die (H13 steel, single cavity): 5-8 weeks
- Multi-cavity H13 tools: 6-8 weeks
More on tool design, steel selection, and ownership: die casting tooling.
First Article and PPAP
After tooling completion, we produce first article samples and submit a full inspection report:
- Full dimensional layout to drawing (all dimensions, all GD&T callouts)
- Material certification (alloy chemistry, mechanical properties)
- Process capability study on all critical features
- Functional test results (pressure test, leak test) if applicable
- PPAP package at Level 1-5 as specified
Nothing moves to production without your formal approval of the first article.
Production with SPC
Approved programs move to production with parameters documented and locked. Injection velocity, peak pressure, die temperature, and cycle time are logged every shot; critical dimensions are measured at defined intervals with SPC charts maintained.
Secondary Operations and Delivery
Parts proceed through CNC machining, surface finishing, and assembly as required by your drawing. They are then packaged to your specification - bulk, tray, individually wrapped, or custom foam - and shipped by ocean or air to your destination.
Manufacturing Capability at a Glance
| Item | Capability |
|---|---|
| Die casting fleet | 16 cold-chamber machines plus hot-chamber zinc cells, 80T-1,600T |
| Magnesium die casting | AZ91D and AM60B on cold-chamber cells, 160T-250T |
| Aluminum alloys | A380, ADC12, A360, A413 |
| Zinc alloys | Zamak 3, Zamak 5, ZA-8 |
| Casting tolerances | CT4-CT6 aluminum (ISO 8062); CT3-CT5 zinc |
| Quality system | ISO 9001:2015 certified; IATF 16949 compliant processes |
| Team and scale | 320+ employees; 12,000+ tonnes annual capacity; 30+ countries served; 20+ years experience |
| Tooling lead times | Prototype single-cavity P20: 3-5 weeks; production single-cavity H13: 5-8 weeks; multi-cavity H13: 6-8 weeks |
| RFQ response | 48 business hours |
Industries and Part Types
| Industry | Representative Custom Parts |
|---|---|
| Automotive / EV | Motor housings, battery tray members, gearbox covers, caliper bodies |
| Industrial Machinery | Hydraulic manifolds, pump housings, motor end shields, compressor crankcases |
| Electronics | Heat sinks, RF shielding enclosures, server chassis components, 5G housings |
| LED Lighting | Streetlight bodies, high-bay housing, floodlight enclosures |
| Consumer Products | Power tool housings, hardware fittings, appliance components |
What to Verify Before Choosing a Custom Die Casting Supplier
A purchasing engineer can verify each point below with a short audit or a targeted phone call:
- In-house tooling vs. sublet - ask who designs and cuts the dies. A supplier with its own tool shop controls lead time, die maintenance, and engineering changes; one that sublets tooling adds a coordination layer to every revision.
- Machining on site - ask whether CNC machining, tapping, and critical-feature finishing happen in the same facility as casting. On-site machining avoids double handling and keeps dimensional responsibility with one team.
- FAI reporting before production release - ask for a sample first article inspection report from a recent program. A supplier that releases production without documented dimensional sign-off transfers that risk to you.
- Export documentation experience - verify familiarity with your Incoterms, packing and labeling expectations, certificates of origin, and alloy material certifications. Documentation errors delay customs clearance more often than casting defects delay orders.
- Tooling ownership terms - get ownership, maintenance responsibility, and transfer terms in writing before paying for a die. Ambiguity here is the most common dispute in custom die casting programs.
What to Send Us
To get started, send any of the following to casting@kastdiecast.com:
- 3D CAD file (STEP, IGES, SolidWorks, PTC) - preferred
- 2D engineering drawing (PDF or DWG) with tolerances
- Physical sample part for reverse engineering
- Sketch or concept - we can provide DFM and design-for-casting advice even at concept stage
Include your target volume, required alloy or application description, and any quality or certification requirements. Submit drawings through the RFQ page and we will respond within 48 business hours.
Materials and Minimum Order Quantities
Aluminum and zinc under one roof. Most custom programs run aluminum (A380, ADC12, A360, A413) for weight and thermal performance; zinc (Zamak 3, Zamak 5, ZA-8) wins for small, thin-walled, high-precision hardware with as-cast threads and plating-friendly surfaces. Material-specific scope: custom aluminum die casting and custom zinc die casting.
Minimum order quantity. There is no fixed MOQ. Share annual volume and we will quote prototype and production tooling separately. Details: low volume die casting.
Lead time. Tooling lead times are listed under In-House Tooling above. Production lead time after PPAP approval is set at program launch and committed in the production agreement - see die casting lead time for the full timeline.
Frequently Asked Questions
Can you handle low-volume prototype programs?
Yes. KastMfg regularly runs prototype programs of 50-500 pieces on P20 prototype tooling at lower cost. Prototype castings come out of the same process and alloy as production - unlike 3D-printed or machined prototypes, they represent the real process and material.
What happens if production parts don't meet my drawing?
KastMfg provides a written non-conformance response within 24 hours of any reported quality issue. We contain the affected inventory, investigate root cause (8D), implement corrective action, and resubmit conforming parts. We do not pass quality problems to the customer.
Can you take over a program currently produced elsewhere?
Yes. We onboard transferred programs regularly. Provide existing tooling for inspection and refurbishment assessment, or supply drawings for new tooling. We qualify the process to your existing PPAP or FAI standard.
Do you have experience with dual-source supply chain requirements?
Yes. Some customers require KastMfg to qualify as a second source while maintaining an existing primary supplier. We support this process with full PPAP submissions and are accustomed to the technical coordination that dual-source qualification requires.
Can you quote from a 3D model without a 2D drawing?
Yes. A 3D model (STEP, IGES, or native CAD) is enough for a budgetary quote and DFM feedback. Before tooling begins we ask for a 2D drawing with tolerances, GD&T callouts, and surface requirements, because die construction and first article inspection are dimensioned against the 2D drawing.
Who owns the tooling?
You do. Ownership is documented in the tooling agreement, and dies are transferable - if you move the program, KastMfg provides the complete die drawings, maintenance records, and the die itself to you or your nominated supplier.
Custom Die Casting & Services
- die casting capabilities
- custom aluminum die casting
- custom zinc die casting
- die casting tooling
- low volume die casting
- prototype die casting
- OEM die casting parts manufacturer
- pressure tight die casting
- die casting assembly service
- die casting CNC machining
- die casting surface finishing services
- zinc die casting plating
- die casting heat treatment
- die casting impregnation
- machining die cast parts
- die casting surface finish options
- large aluminum die casting
- die casting automation
- investment casting - steel, stainless, and complex geometry when HPDC is not suitable
- investment casting services
Start your custom program: casting@kastdiecast.com | +86 138 1403 4409 | No.6, Rungu Road, Nanjing, China
Related Resources
Next steps for custom die casting
Die Casting Tooling & Mold Design | H13, P20 Steel
Die casting tooling designed and manufactured in-house using H13 and P20 tool steel. Prototype and production dies, mold maintenance, and tool transfer.
ServiceAluminum Die Casting Manufacturer | A380 & ADC12
Custom aluminum die casting in A380, ADC12, A360 & A413: 160T-1,600T presses, 12,000+ tonnes/year, CT4-CT6 tolerances, in-house machining & finishing.
CapabilityQuality Control
Review inspection workflow, traceability support, and process control standards before launch.
Process GuideDie Casting Process
See how casting, trimming, machining, finishing, and inspection fit together in production.
Next StepRequest a Quote
Send your drawing package and target volume to get an engineering-backed quotation.
Need a Quote for Your Project?
Our engineering team is ready to review your requirements and provide competitive pricing with fast turnaround.
Request a Quote